STERILIZATION OF PACKAGED PRODUCTS – THE SECRET TO MAINTAINING QUALITY AND SAFETY
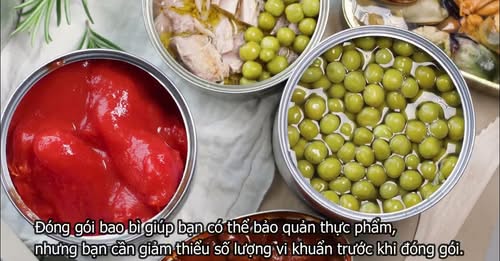
Sterilizing canned, bottled, or sealed packaged foods not only ensures food safety and hygiene but also preserves natural flavors and colors. That is why the modern food processing industry cannot function without advanced sterilization equipment!
✨ Sterilization Process – The Pinnacle of Preservation Technology:
After packaging, products are placed into a sterilizer and heated under high pressure at temperatures of 121°C – 135°C for approximately 5 - 120 minutes, depending on the characteristics of the food. For optimal efficiency, factors such as:
✔ Temperature
✔ Heating and cooling times
✔ Sterilization time must be precisely calculated.
This not only reduces production costs but also ensures superior quality, helping products win over consumers.
✨ ALP Retort RKZ-40II – Comprehensive Sterilization Solution
The ALP Retort Autoclave Model RKZ-40II is the perfect choice for both the food industry and R&D laboratories, featuring outstanding highlights:
⏩ Capacity: 96 liters
⏩ Sterilization temperature: 60°C – 121°C
⏩ Maximum pressure: 0.170 Mpa
⏩ Technological advantages:
Stable temperature and pressure control, ensuring packaging is not deformed.
Compatible with a wide range of modern packaging materials and processes.
✨ Outstanding features of RKZ-40II:
✅ Precise pressure-controlling air compressor
✅ Two customizable cooling modes
✅ Automatic operation with just one Start button
✅ Integrated temperature sensors and dedicated data logger
✅ Meets F-value standards